

Patented · Innovative · Green
Innovations
Patent
Patented Hybrid Wood™ Technology
LESS GLUE. MORE WOOD. A HEALTHIER HOME.
Conventional multilayer engineered flooring bonds every veneer with glue that may contain formaldehyde. A typical 2,000 sq ft home floored with traditional 9-ply engineered wood can carry up to 16,000 sq ft of formaldehyde-based glue (2,000 sq ft × 8 glue layers). That is a lot of unnecessary exposure in your home.
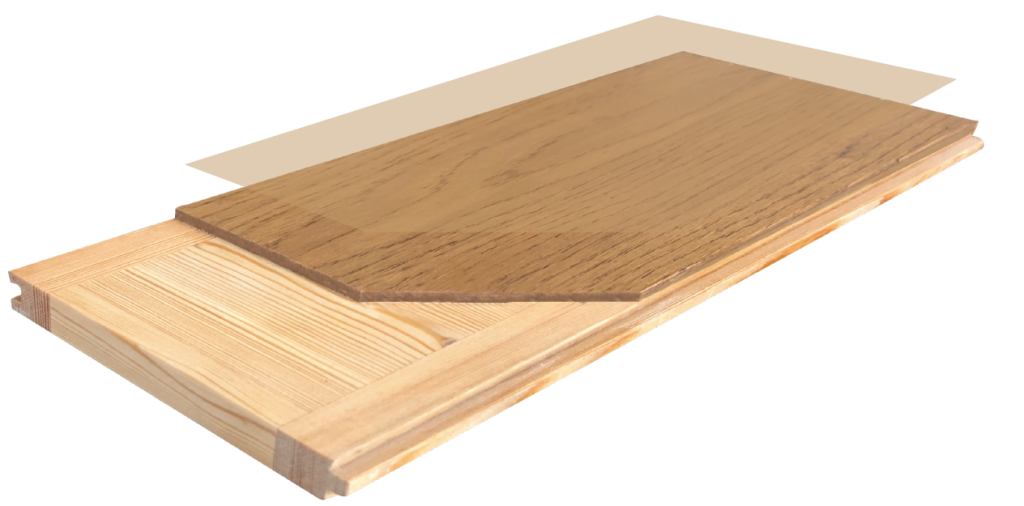
Alston’s patented HYBRID WOOD™ technology reinvents how a floor is built: ONE layer of formaldehyde-free adhesive, 100% natural solid wood, and CARB NAF-certified, zero-VOC materials. Precision-engineered cross-grain solid wood fillets and structural edge beams deliver exceptional strength and dimensional stability. The result is a stronger, more stable hardwood floor made with your family’s well-being and the environment in mind, without giving up the natural beauty of real wood.
ALSTON HYBRID WOOD™ — Engineered Smarter. Built Better. Naturally.
U.S. Patent #: US9340984B2
-
Durability
Up to 11 layers of Exclusive Diamond Class "Anti-Scratch" and "Anti-Abrasive", Ceramic UV Modified-Oil finishes to provide the maximum protection against daily usage. No re-oiling is needed.
-
Wearability
4mm-thick Natural Hardwood Veneer Wear Layer, allows for multiple refinishing and sanding.
-
Health & Safety
CARB NAF Certified, 100% Natural Wood engineered with Formaldehyde-FREE adhesives and Zero-VOC materials makes this a Top Eco-Friendly GREEN Product.
-
Stability
Revolutionary Natural Wood Cross-Grain Fillets and Structural Edge Beams Interlocking Construction, combined with an "Anti-Moisture" sealer process for moisture protection, ensures optimal Dimensional Stability.
Innovation
A stronger, more stable floor
This innovative 2-ply construction brings together the natural beauty of real hardwood, advanced engineering, and thoughtfully selected, health-conscious materials for a stronger, more stable, and healthier flooring solution.
Revolutionary Innovation
- Patented 2-Ply Engineered Technology – Innovative Engineering with Health-Conscious Materials
- Interlocking Construction – Reinforced with Cross-Grain Lumber Fillets and Structural Edge Beams
- Enhanced Hardwood Wear Layer – Built Over a Pine Wood Foundation for Advanced Stability
- 100% Natural Wood Product – Safe, Sustainable, and VOC-Free
Superior Advantages
- Enduring DURABILITY
- Advanced STABILITY
- Excellent WEARABILITY
- Enhanced LIVABILITY
Green
The Healthiest Flooring Available
CARB NAF Certified, 100% Natural Wood engineered with Formaldehyde-FREE adhesives and Zero-VOC materials makes this a Top Eco-Friendly GREEN Product.
-
CARB NAF
No Added Formaldehyde. The strictest California air standard for wood products.
-
FSC
Forest Stewardship Council. Wood from responsibly managed forests.
-
ISO 14001
Environmental management. Our factories track and reduce their impact.


What we make
Flooring, trim and the pieces in between
Alston manufactures, imports and distributes its own hardwood, waterproof StoneCoreX SPC and laminate flooring, with factory-matched trims, moldings and stair parts.
We also produce hand-crafted architectural wood carvings and other building materials to order.
Ready to Define Your Space
Join our network of elite architects and interior designers who trust Alston for their most prestigious project